In the field of high-performance advanced high-strength steel structures, the choice of precision “low-temperature tempering (typically 150 °C – 250 °C)” for S690-grade structural steel sections (e.g. S690QL, S690M) before delivery is the core quench-and-temper technology breakthrough.
When these sections are further precision-manufactured using the automated laser welding (Laser Fused) technology introduced by Peak Kong Special Steel, the material’s physical limits and geometric precision are pushed to entirely new heights.
The following breaks down the four core advantages of S690 section low-temperature tempering and the process revolution brought by laser welding:
Substantially lowering the initial Y/T ratio, ensuring seismic plastic energy-dissipation space:Conventional high-temperature tempering pain point: As tempering temperature rises, tensile strength drops far faster than yield strength, causing Y/T to rise instead (often > 0.93, approaching 0.96), meaning the material faces sudden brittle fracture immediately after yielding — extremely dangerous in seismic design of buildings and bridges. Low-temperature tempering solution: It perfectly retains extremely high-density dislocations in the matrix, or stabilises 5%–15% thin-film metastable retained austenite. When the section is loaded past the yield point, intense dynamic dislocation tangling and TRIP effect are triggered, significantly raising tensile strength, successfully lowering Y/T to around 0.85–0.88 while pushing total elongation to 17%–20% or above. This golden combination provides the plastic deformation energy-dissipation space critical for highway bridges and high-rise buildings.
Precision control of micro-hardness and internal stress, preventing section brittle self-cracking:Quenching aftereffects: To lock in ultra-high strength, steel undergoes rapid water quenching, fully transforming internal structure to martensite. Freshly quenched martensite accumulates enormous thermal and structural stress, extremely prone to spontaneous brittle cracking. Low-temperature tempering benefit: Per EN 1011-2 stress control logic, 150 °C–250 °C tempering, while not damaging the 690 MPa yield strength base, is sufficient to allow locally strained carbon atoms to microscopically rearrange, releasing over 80% of quenching residual stress. This controls the section’s micro-hardness and internal stress below the critical safety line recommended by the standard, blocking the root cause of brittle self-cracking.
Enhancing microstructural thermal stability, suppressing catastrophic HAZ softening:Conventional pain point: If steel is delivered with conventional medium-high-temperature tempering, the HAZ during site welding easily undergoes severe secondary grain coarsening and excessive martensite decomposition, forming a deadly “softening zone” that drastically reduces overall joint strength. Low-temperature tempering defence: The mill’s low-temperature tempering locks in the fine-grained microstructure barrier, significantly enhancing the matrix’s thermal stability. When low-heat-input narrow-bead welding (e.g. robotic auto-weld, FCAW, or CMT Cold Metal Transfer) compliant with EN 1011 is used, HAZ softening and embrittlement are minimised, ensuring max HAZ hardness ≤ 450 HV with no severe softening, and joint strength 100% meeting the most stringent infrastructure acceptance criteria.
Locking in geometric precision, stabilising long-term service dimensions of structural sections:Eliminating service hazards: Retained austenite and non-equilibrium martensite from water quenching are unstable phases that spontaneously and slowly transform with volume expansion during long-term ambient storage or service loading, causing slight section warping. Locking in precision: The mill’s low-temperature tempering causes these unstable microstructures to complete their microscopic transformation early, locking in the geometric dimensions and cross-sectional precision of structural sections, ensuring that in high-rise building mega-columns or deep foundation piling, no geometric distortion occurs over decades of service.
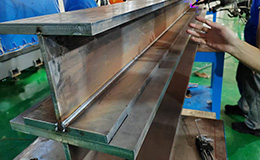
Conventional high-performance steel is mostly delivered as plates; secondary cold forming in the workshop is extremely difficult and prone to springback and cracking that destroy elongation. Peak Kong Special Steel adopts top-tier automated laser welding technology to directly prefabricate low-temperature-tempered S690 high-strength steel plates into a full range of structural long sections and hollow sections:
Ultimate “depth-to-width ratio” and low heat input: Laser welding energy is highly concentrated; the weld is deep and narrow, with heat input far lower than conventional arc welding. This compresses the HAZ to the extreme, perfectly preserving the low Y/T (0.85–0.88) and high elongation (≥17%) microstructure obtained through low-temperature tempering.
Near-zero-deformation geometric cross-sections: With minimal welding thermal deformation, Peak Kong’s prefabricated H-beams, Universal Columns/Universal Beams (UC/UB), piling H-beams, square hollow sections (SHS), rectangular hollow sections (RHS), and circular hollow sections (CHS) have near-perfect straightness and cross-sectional precision, ready for direct site installation.
Although the material has excellent properties, when these S690 laser-welded sections arrive at your workshop or site for secondary processing, the following iron rules must be strictly enforced per EN 1011:
Conventional PWHT (post-weld heat treatment) strictly prohibited:Overall stress-relief annealing (e.g. conventional 600 °C furnace annealing) of members is absolutely not permitted. Medium-high-temperature heating in the workshop would completely destroy the ultra-fine-grained microstructure stabilised by low-temperature tempering, directly dropping yield strength by 20%–30%.
Flame heat straightening (hot straightening) strictly prohibited:After welding deformation, high-temperature flame torches for local heating and hammer straightening of S690 sections are absolutely prohibited.
-
 2026-6-16 S960QL Ultra-High Strength Structural Steel Profiles
-
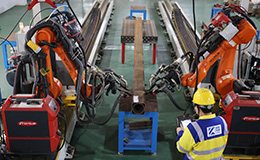 2026-9-03 Introduction to High-Strength Steel Structures
-
 2025-12-19 Peak Kong Special Steel will participate in the 2025 Stainless Steel World Expo in the Netherlands
-
 2025-1-06 The welding team at Peak Kong Special Steel has successfully completed the welding procedure qualification for duplex stainless steel and super duplex stainless steel 2205/2507.
-
2026-9-17 Who Are the Suppliers of S690 High-Performance Structural Steel Sections?
-
 2026-6-16 Composite Hollow Structural Profiles – The Future of Structures
-
 2024-12-06 Peak Kong Special Steel Showcases Advanced High-Strength Steel Structural Profiles at WCFS International Conference